Case Study: Setting Up a Complete PET Preform Production Line for a Client in Southeast Asia
A Turnkey Engineering Analysis on High-Cavitation Tooling, Auxiliary Integration, and Environmental Adaptation by GTWMOULD
Executive Summary: Expanding High-Speed Bottling Capabilities in Tropical Climates
The beverage market across Southeast Asia demands ultra-reliable, high-capacity Polyethylene Terephthalate (PET) packaging solutions capable of operating continuously in high-ambient temperature and humidity environments. A prominent regional beverage converter partnered with GTWMOULD—a leading Chinese precision manufacturer specializing in high-performance PET preform mold engineering—to design, commission, and optimize an end-to-end 72-cavity PET preform production line.
This technical case study explores how GTWMOULD delivered a complete turnkey solution, integrating FEA-optimized hot runner systems, climate-adapted mold cooling, sub-micron core alignment, and automated downstream handling to achieve exceptional productivity and zero-defect quality.
1. Client Challenge & Operational Environment
The Southeast Asian packaging converter faced severe operational hurdles with their existing supplier equipment, resulting in low production efficiency and high scrap rates under tropical manufacturing conditions:
- High Ambient Humidity & Sweating: Continuous surface condensation (sweating) on mold cavities caused water drop marks, silver splay streaks, and hydrolytic polymer degradation.
- Unstable Multi-Cavity Filling: Unbalanced melt flow led to frequent peripheral short shots and inconsistent shot-to-shot preform weights.
- Severe Thermal Hazing & AA Accumulation: Inadequate gate quenching in humid ambient plant air produced milky crystallization around the gate zone and elevated Acetaldehyde (AA) levels ($> 3.2 \text{ ppm}$).
- Frequent Down-Time: Mechanical alignment shifts during thermal expansion caused neck split flash and thread ovality.
2. The Integrated Turnkey System Architecture
GTWMOULD engineered a fully synchronized, turnkey PET preform production line customized for high-humidity, high-throughput operating conditions:
| System Module | Engineering Specification | GTWMOULD Custom Adaptation |
|---|---|---|
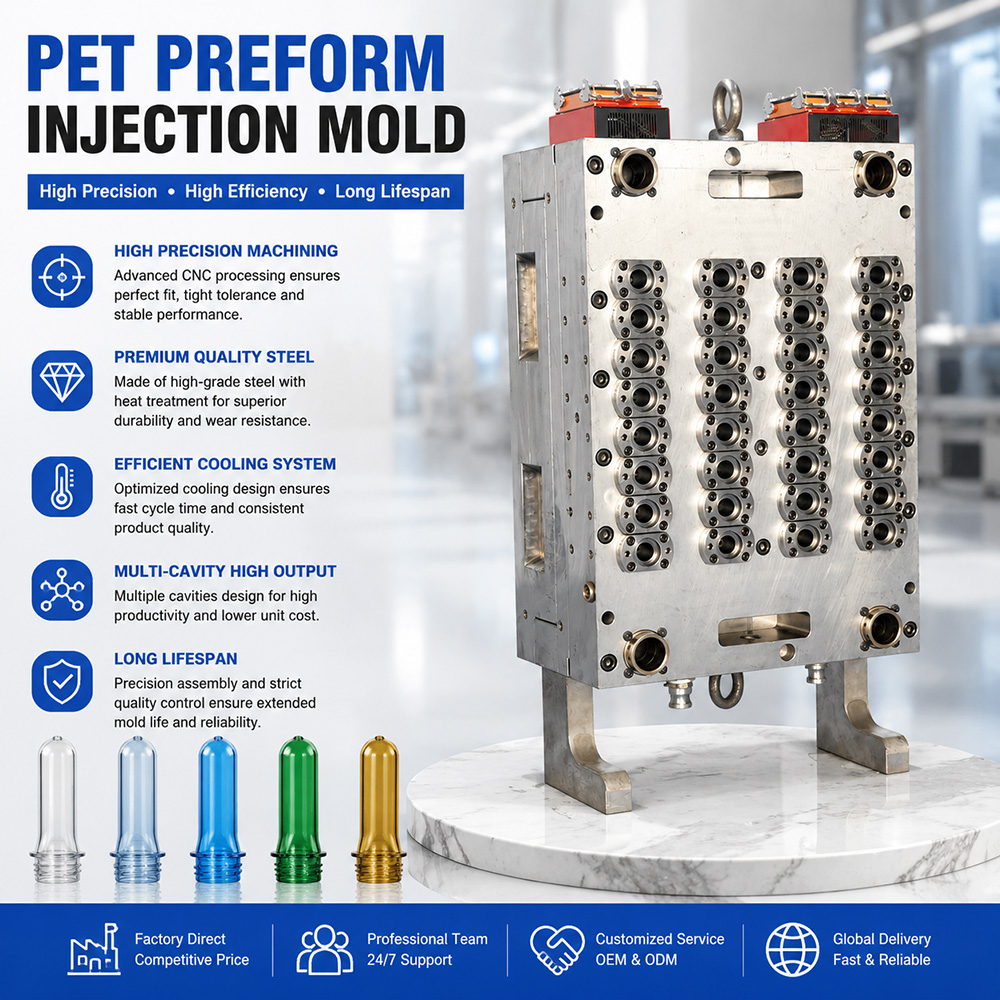
| High-Cavitation Tooling | 72-Cavity Valve Gate PET Preform Mold (28mm PCO 1881, 14.5g) | Swedish S136 stainless cavity stacks ($48\text{--}52 \text{ HRC}$) with triple-taper self-locking alignment. |
| Hot Runner System | 72-Drop Valve Gate Naturally Balanced Hot Runner Manifold | Micro-polished, equal-length flow channels with independent pneumatic pin actuation. |
| Mold Dehumidification | Closed-Loop Enclosure Dehumidifier ($< -10^\circ\text{C}$ Dew Point) | Eliminates mold sweating and surface moisture splay under $38^\circ\text{C}$ ambient plant conditions. |
| Thermal Management | High-Velocity Chiller & High-Pitch Spiral Cavity Loops | Press-fitted Beryllium-Copper (BeCu) inserts at gate and neck zone for rapid thermal quenching. |
| Downstream Automation | 3-Axis Post-Mold Cooling Robot & Vision Inspection | Water-cooled take-out plate with internal core cooling tubes to prevent post-ejection deformation. |
3. Engineering Interventions and Key Technical Innovations
1. Triple-Taper Alignment to Prevent Concentricity Shift
Thermal expansion variations in tropical plants can cause core pins to shift out of alignment under high injection pressures ($1100\text{--}1400 \text{ bar}$). GTWMOULD incorporated a proprietary triple-taper self-locking component alignment system across core, cavity, and neck split components. This locks the core-to-cavity concentricity strictly within:
$$\Delta \le 0.015 \text{ mm}$$
This maintained total wall thickness variation under $0.025 \text{ mm}$ across all 72 cavities, completely eliminating thin-wall blowout defects during downstream stretch blow molding.
2. Advanced Thermal Quenching & BeCu Inserts
To freeze the molten polymer below its glass transition temperature ($T_g \approx 75\text{--}80^\circ\text{C}$) before crystalline spherulites could form, GTWMOULD integrated high-pitch spiral cooling channels around cavity inserts alongside hyper-conductive Beryllium-Copper (BeCu) gate blocks. BeCu dissipates heat up to 10x faster than standard steel, eliminating gate hazing and keeping AA levels well below strict still-water packaging limits ($< 1.8 \text{ ppm}$).
3. Environmental Anti-Sweat Enclosure
To defeat Southeast Asia's high atmospheric humidity, GTWMOULD supplied an integrated mold enclosure paired with a continuous dry-air dehumidification unit. By maintaining a dry micro-environment around the parting line, chilled water ($6\text{--}8^\circ\text{C}$) can run continuously without condensation, securing uninterrupted 24/7 manufacturing.
4. Quantified Project Results and Operational ROI
Upon final commissioning and performance qualification testing at the client's facility in Southeast Asia, the turnkey GTWMOULD line achieved outstanding operational metrics:
- Cycle Time Reduction: Total injection cycle time compressed from a baseline of 13.8 seconds down to 10.2 seconds.
- Rejection Rate Drop: Overall preform scrap rate decreased from 5.8% to under 0.12%.
- Output Acceleration: Daily preform production increased by over 32%, delivering an additional 180,000 units per day.
- Zero Condensation Downtime: Continuous 24-hour operation achieved without sweat-related surface marks or tool rust scaling.
Conclusion: GTWMOULD — Global PET Preform Solutions Partner
This case study demonstrates that establishing an efficient high-volume preform manufacturing facility in challenging environments requires deeply integrated turnkey engineering. By mastering sub-micron component alignment, balanced hot runner dynamics, thermal quenching, and micro-climate control, GTWMOULD empowers beverage producers worldwide to achieve maximum operational efficiency and lowest unit cost.
Contact GTWMOULD's engineering experts today to discuss turnkey PET preform production line setups customized to your regional manufacturing needs.